Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124
Physical Address
304 North Cardinal St.
Dorchester Center, MA 02124


UV and Ozone are two of the most powerful oxidants used in modern water treatment. When we pair them, we create an advanced oxidation process (AOP) that can tackle contaminants that single‑treatment methods struggle to remove.
UV radiation generates highly reactive hydroxyl radicals when it interacts with ozone, dramatically increasing the oxidative capacity of the system. Ozone alone already destroys many organic molecules, but the addition of UV accelerates the reaction rate and expands the range of target pollutants.
We also benefit from a synergistic effect on disinfection. UV photons inactivate microorganisms by damaging their DNA, while ozone oxidizes cell membranes and intracellular components, providing a double layer of protection.
Finally, the combined approach can reduce chemical dosing and operational costs. Because the reaction proceeds more quickly, we often need less ozone to achieve the same level of treatment, which translates into lower energy consumption and fewer by‑products.
When ozone (O₃) absorbs UV light at 185 nm, it splits into molecular oxygen and an oxygen atom, which quickly forms the hydroxyl radical (·OH). The hydroxyl radical is the most potent oxidant known, with a redox potential of about 2.8 V, far exceeding that of ozone (2.1 V). This increase in potential allows the system to break down stubborn compounds such as pesticides, pharmaceuticals, and endocrine‑disrupting chemicals.
We have observed that the presence of UV can cut the half‑life of many contaminants by up to 70 % compared with ozone alone. Shorter half‑lives mean that water spends less time in the reactor, which can shrink the footprint of the treatment plant. Moreover, the rapid oxidation reduces the formation of secondary by‑products that sometimes arise from slower reactions.
In practice, the enhanced oxidation translates into higher compliance with regulatory limits for total organic carbon (TOC) and chemical oxygen demand (COD). Facilities that adopt UV‑ozone AOPs often report TOC reductions of 85 % or more, a performance level that is difficult to achieve with conventional disinfection alone.
UV‑ozone AOPs are effective against a wide range of contaminants, from simple microbes to complex organic molecules. For instance, the system can mineralize chlorinated solvents, which are notoriously resistant to standard oxidation processes. The same technology also degrades volatile organic compounds (VOCs) that can cause odor and taste issues in drinking water.
We have found that the combined process works well for emerging contaminants such as per‑ and polyfluoroalkyl substances (PFAS). While PFAS are highly stable, the intense oxidative environment created by UV‑activated ozone can break the carbon‑fluorine bonds, leading to shorter‑chain fragments that are easier to remove in downstream treatment steps.
Because the process does not rely on a single mechanism, it offers flexibility for different water sources. Whether we treat surface water with high turbidity or reclaimed wastewater with trace pharmaceuticals, the UV‑ozone AOP can be tuned to meet the specific challenge.
Energy consumption is a key metric for any treatment technology. UV lamps consume electricity, but the amount of ozone required is often reduced by 30 %–50 % when the two are combined. This offset can make the overall energy use comparable to, or even lower than, standalone ozone or UV systems.
We also appreciate the reduced need for chemical additives. Traditional advanced oxidation processes sometimes require hydrogen peroxide or persulfate, which add handling and storage costs. UV‑ozone AOPs rely solely on the two oxidants we already generate on‑site, simplifying logistics.
Maintenance is streamlined because the system uses a single reactor vessel for both UV and ozone contact. This design minimizes the number of pressure vessels, pumps, and control loops, which in turn lowers the risk of mechanical failure and simplifies routine inspections.
When we design a UV‑ozone AOP, we start by matching the UV dose to the ozone concentration to achieve the desired radical generation rate. The reactor geometry, flow pattern, and lamp placement all influence the contact time and the uniformity of exposure.
Materials selection is another critical factor. Ozone is a strong oxidizer, so we use corrosion‑resistant alloys such as Hastelloy or PTFE‑lined components to protect the reactor and piping. UV lamps are typically made of quartz, which resists ozone attack while allowing high transmission of the 185 nm wavelength.
Control systems must monitor both UV intensity and ozone output in real time. Sensors for UV irradiance, ozone concentration, and residual oxidant levels feed into a programmable logic controller (PLC) that can adjust lamp power or ozone flow to maintain optimal performance.
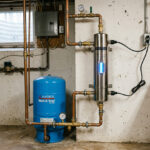
One common design is the annular reactor, where a UV lamp sits at the center of a cylindrical chamber and ozone is introduced tangentially. This arrangement creates a swirling flow that enhances mixing and ensures that every water parcel receives sufficient UV exposure.
Alternatively, we may employ a flat‑plate reactor for high‑throughput applications. In this setup, UV lamps are mounted on both sides of a thin water film, and ozone is diffused through a porous membrane. The short path length maximizes photon utilization and reduces the required lamp power.
We also consider modular reactors for retrofits. These units can be added to existing treatment trains without major civil works, allowing facilities to upgrade their oxidation capacity incrementally.
Low‑pressure mercury lamps emit strong peaks at 185 nm and 254 nm, making them ideal for ozone activation and microbial inactivation, However, they have a limited lifespan and require periodic replacement.
We sometimes opt for medium‑pressure lamps, which produce a broader spectrum and higher photon flux, but they generate more heat and may need additional cooling. The choice depends on the specific contaminant profile and the desired treatment speed.
Regular cleaning of lamp sleeves is essential to maintain UV transmittance. Ozone can degrade organic fouling, yet mineral scaling may still occur, especially in hard water. Automated cleaning cycles using acid or citric‑based solutions can keep the system operating at peak efficiency.
We generate ozone on‑site using a corona discharge ozone generator, which converts a portion of the feed air or oxygen into O₃. The generator’s output is typically measured in grams per hour (g/h) and adjusted based on the required dose.
To protect downstream equipment, we use ozone destructors or catalytic converters to remove excess ozone before the water leaves the reactor. This step prevents ozone off‑gassing into the atmosphere and ensures compliance with occupational safety standards.
Proper venting and monitoring of ozone concentrations in the plant air are mandatory. Portable ozone detectors and fixed‑point analyzers provide continuous feedback, allowing us to intervene quickly if levels approach regulatory limits.
We evaluate UV‑ozone AOPs using a suite of analytical methods that quantify oxidant demand, contaminant removal, and by‑product formation. Key performance indicators include COD reduction, TOC removal, and log‑reduction values (LRVs) for pathogens.
Laboratory bench‑scale studies help us optimize the UV dose and ozone concentration before scaling up. Pilot trials in real water matrices confirm that the laboratory results translate to field conditions.
Regulatory compliance is verified through regular sampling and reporting. We often work with third‑party laboratories to certify that the treatment meets drinking water standards set by the EPA, WHO, or local authorities.
| Contaminant Type | Removal Efficiency (UV‑Ozone AOP) | Typical Dose (UV mJ/cm² / O₃ mg/L) |
|---|---|---|
| Escherichia coli | ≥ 5 log | 40 mJ/cm² / 0.5 mg/L |
| Cryptosporidium oocysts | ≥ 3 log | 60 mJ/cm² / 0.8 mg/L |
| Trihalomethanes (THMs) | 90 %–95 % | 50 mJ/cm² / 1.0 mg/L |
| PFAS (C8) | 70 %–80 % | 80 mJ/cm² / 1.5 mg/L |
| Pharmaceuticals (e.g., ibuprofen) | 85 %–92 % | 45 mJ/cm² / 0.7 mg/L |
These figures represent averages from multiple pilot studies and may vary with water chemistry, temperature, and hydraulic retention time.
Residual ozone and UV transmittance are measured at the reactor outlet to ensure that the process has achieved the target oxidation level. We use an ozone analyzer based on UV absorption at 254 nm, which provides rapid feedback on residual concentration.
UV intensity is monitored with a calibrated radiometer that reports irradiance in milliwatts per square centimeter (mW/cm²). Continuous logging allows us to detect lamp aging or fouling before performance degrades.
When residual oxidants exceed design limits, we adjust the ozone feed or increase the UV dose through the PLC. This closed‑loop control maintains consistent water quality across fluctuating influent conditions.
One concern with strong oxidation is the formation of bromate when bromide is present in the source water. To mitigate this, we monitor bromide levels and, if necessary, lower the UV dose or add a scavenger such as bisulfite.
We also track the formation of aldehydes and ketones that can arise from partial oxidation of organic matter. Advanced analytical techniques like gas chromatography‑mass spectrometry (GC‑MS) help us identify and quantify these intermediates.
When by‑products are detected above acceptable thresholds, we can introduce a post‑treatment step such as activated carbon adsorption or biological filtration to polish the water before distribution.
Our experience spans municipal drinking water plants, industrial wastewater facilities, and swimming‑pool sanitation systems. Each case demonstrates how the UV‑ozone AOP can be tailored to specific regulatory and operational goals.
Below we highlight three representative projects that illustrate the versatility and impact of the combined technology.
The city of Riverton faced rising levels of chlorination by‑products and emerging contaminants in its source reservoir. We installed a UV‑ozone AOP with a capacity of 5 MGD, integrating it after the conventional coagulation‑flocculation train.
After six months of operation, the plant reported a 92 % reduction in total organic carbon and a 98 % drop in trihalomethanes. The UV dose was set at 45 mJ/cm², while ozone was dosed at 0.9 mg/L, achieving the target oxidation without exceeding bromate limits.
Operational costs decreased by 12 % compared with the previous system that relied on chlorine and UV alone, mainly due to lower chemical purchases and reduced sludge generation.
A pharmaceutical producer needed to treat effluent containing trace amounts of active pharmaceutical ingredients (APIs) such as carbamazepine and diclofenac. A UV‑ozone AOP was chosen because the contaminants are resistant to conventional biological treatment.
The pilot plant operated at a flow rate of 2 m³/h, using a medium‑pressure UV lamp delivering 70 mJ/cm² and an ozone dose of 1.2 mg/L. Laboratory analysis showed removal efficiencies of 94 % for carbamazepine and 90 % for diclofenac, bringing concentrations below the discharge limits.
Because the process generated minimal sludge, the facility avoided costly waste‑handling fees, and the overall energy consumption was comparable to its existing UV‑only system.
A resort with multiple outdoor pools sought a chlorine‑free solution that would reduce skin irritation for guests. We recommended a compact UV‑ozone system that could be retrofitted onto the existing recirculation loop.
The system delivered a UV dose of 30 mJ/cm² and an ozone concentration of 0.6 mg/L, achieving a 5‑log reduction of Legionella and a 4‑log reduction of Pseudomonas aeruginosa. Water quality tests confirmed the absence of residual chlorine and a clear, odor‑free pool environment.
Guest satisfaction scores rose by 15 % after implementation, and the resort reported a 20 % reduction in chemical procurement costs.
The main benefit is the creation of hydroxyl radicals, which are far more reactive than either UV or ozone alone. This leads to faster and more complete oxidation of difficult‑to‑treat contaminants.
In addition, the combined system can achieve higher disinfection log‑reduction values while using less ozone, which reduces both chemical costs and the risk of bromate formation.
Overall, the synergy improves treatment performance without requiring a proportional increase in energy consumption.
Yes, many municipalities have adopted the technology to meet stringent drinking‑water standards. It is especially effective for removing organic micropollutants, taste‑and‑odor compounds, and residual disinfectants.
Regulators often require documentation of by‑product levels, and the UV‑ozone process can be tuned to keep bromate and aldehyde formation within acceptable limits.
When integrated with conventional treatment steps, the AOP can serve as a polishing stage that ensures safe, high‑quality water for consumers.
Safety is built into the design through ozone destructors, ventilation, and continuous monitoring of ambient ozone concentrations. Operators are protected from direct exposure to UV radiation by shielding and interlock mechanisms that shut down lamps if a cover is removed.
Training on proper maintenance, such as lamp replacement and ozone generator servicing, further reduces risk. The system also includes alarms that alert staff to any deviation from safe operating parameters.
Overall, when installed and operated according to manufacturer guidelines, the technology poses minimal health hazards.
Because the combined process requires less ozone to achieve the same oxidation level, the energy used by the ozone generator can be reduced by up to 40 %. The UV lamp power may be similar to a standalone UV system, but the overall energy footprint is often lower due to the reduced ozone demand.
Field data from several installations show a net energy saving of 10 %–15 % compared with running two independent units in parallel.
These savings become more pronounced at larger scales, where the cost of electricity and ozone generation represents a significant portion of operating expenses.
Regular cleaning of UV lamp sleeves is critical to maintain high transmittance. Depending on water quality, cleaning may be required weekly or monthly.
Ozone generators need periodic inspection of the dielectric plates and replacement of worn electrodes. Additionally, ozone destructors should be checked for catalyst activity and replaced according to the manufacturer’s schedule.
Finally, calibration of UV and ozone sensors should be performed at least annually to ensure accurate feedback for the control system.
Yes, modular reactors are available that can be inserted into existing pipelines with minimal disruption. These units often come with pre‑wired control panels that integrate with the plant’s SCADA system.
Retrofitting typically involves adding a UV lamp housing, an ozone injection point, and the necessary instrumentation. The footprint of a modular unit is usually comparable to that of a standard oxidation tank.
Because the technology does not require major structural changes, many facilities choose retrofitting as a cost‑effective path to upgrade their oxidation capacity.
One limitation is the potential formation of bromate when bromide concentrations are high. Careful control of UV dose and ozone concentration, along with bromide monitoring, is required to keep bromate below regulatory limits.
Another consideration is the initial capital cost of UV lamps and ozone generators, which can be higher than single‑process systems. However, the long‑term operational savings often offset this upfront investment.
Finally, the process is less effective in highly turbid water unless pre‑filtration is employed to remove suspended solids that can shield UV light.
We have a comprehensive guide that covers the fundamentals, design considerations, and safety practices for ozone water treatment. You can explore it at Ozone Water Treatment Guide.
Yes, our pool‑ozone system guide provides step‑by‑step instructions for selecting, installing, and maintaining ozone units for swimming‑pool applications. Visit Pool Ozone System Guide for more information.
Ozone is a powerful oxidant, but when used correctly it is safe for residential water treatment. Our safety overview explains the precautions and best practices for home installations. See Is Ozone Water Treatment Safe? for details.
Selection depends on the target contaminant, required UV dose, and the presence of ozone. Low‑pressure lamps are ideal for 185 nm activation of ozone, while medium‑pressure lamps provide higher photon flux for broader applications.
We recommend consulting our technical team to evaluate your water quality and treatment goals before making a final decision.
With proper maintenance, UV lamps typically last 8 000–12 000 hours, and ozone generators can operate reliably for 5–7 years before major component replacement is needed.
Regular cleaning, monitoring, and scheduled part replacements extend the overall system life and ensure consistent performance.
Yes, modern control systems can adjust ozone flow and UV intensity in real time to accommodate fluctuations in influent flow. This flexibility helps maintain treatment efficacy during peak demand periods.
Hydraulic design, such as using variable‑speed pumps and flow‑control valves, further enhances the system’s ability to cope with changing conditions.
Ozone decomposes back to oxygen, leaving no persistent chemical residues in the treated water. This makes it an environmentally friendly oxidant compared with chlorine, which can form chlorinated by‑products.
However, ozone off‑gassing must be managed to avoid atmospheric release, which is why ozone destructors and proper ventilation are integral to system design.
Initial capital costs are higher, but operational expenses are often lower due to reduced chemical purchases and lower sludge handling fees. Over a 10‑year horizon, many facilities find the total cost of ownership to be comparable or even favorable.
Additionally, the ability to meet stricter regulatory limits without additional treatment steps can provide long‑term financial benefits.
Absolutely. It can serve as a pre‑treatment for membrane filtration, a post‑treatment for biological processes, or a standalone polishing step before distribution.
Integration with advanced sensors and automation platforms allows seamless coordination with existing plant infrastructure.
Systems should comply with IEC 60825‑1 for laser and UV safety, as well as ISO 9001 for quality management. Ozone generators must meet EPA and local environmental regulations regarding ozone emissions.
Third‑party testing and certification, such as NSF/ANSI 61 for drinking‑water components, provide additional assurance of safety and performance.
Our engineering team conducts a site‑specific assessment that includes water quality analysis, flow‑rate calculations, and space constraints. Based on this data, we develop a tailored UV‑ozone AOP design that meets your performance and budget goals.
Contact us through our website to schedule a consultation and receive a detailed proposal.
By harnessing the complementary strengths of UV radiation and ozone, we can achieve a level of water purification that meets today’s demanding regulatory and consumer expectations. The advanced oxidation process we have described offers flexibility, efficiency, and safety across a wide range of applications.
Whether you are upgrading a municipal plant, refining industrial effluent, or seeking a chlorine‑free pool solution, the UV‑ozone AOP provides a robust pathway to cleaner, safer water.
Sarah Mitchell holds a degree in Environmental Science and has spent the last decade covering water treatment technology and regulations. She leads the editorial team at delozone.com, ensuring every article meets the highest standards of accuracy and sourcing.